PCBA Quality Assurance for Buyers Who Need Release Evidence
PCBInsider builds quality assurance around evidence buyers can review: first article inspection, IPC-A-610 workmanship checks, PFMEA-linked control plans, 8D corrective action, and inspection records tied to the released PCB assembly revision.
Quality Assurance Starts Before the First Board Is Released
PCBA quality assurance is a controlled release system, not a final inspection label. A buyer should be able to see which revision was built, which inspection criteria were used, what defects were found, how suspect units were contained, and which production controls changed before the next lot.
The strongest programs connect first article inspection, failure mode and effects analysis, and 8D problem solving into one practical manufacturing loop. That is the gap this service fills between standard PCB assembly and a buyer-ready release package.
FAI Report Built Around the Released Package
First article inspection checks the first production-representative PCBA against the released Gerber, BOM, centroid data, assembly drawing, polarity notes.
PFMEA and Control Plan Alignment
PFMEA review connects expected process risks to inspection and test gates instead of leaving quality checks as generic steps.
8D Corrective Action for Escapes and Repeat Defects
8D reporting gives buyers a disciplined format for containment, root cause, permanent correction, and recurrence prevention.
Inspection Gates Matched to Package Risk
AOI is strong for visible parts, X-ray is needed for BGA and bottom-terminated packages, and ICT or functional test confirms electrical behavior.
Revision and Deviation Control
Quality records lose value when the build revision is unclear.
Lot Feedback That Improves the Next Build
Quality assurance should produce line learning, not only pass/fail status.
PCBA Quality Assurance Scope and Limits
Best-fit quality profile
This service is strongest when a buyer needs documented approval gates for a PCBA that will repeat after prototype or pilot build. For a one-off hobby board, full FAI and 8D paperwork may add cost without enough risk reduction.
Which Quality Record Solves Which Buyer Problem?
FAI, PFMEA, control plans, and 8D reports are often requested as a bundle, but each record answers a different commercial question. Treating them separately prevents paperwork from replacing actual process control.
| Record | Buyer question answered | When to request it |
|---|---|---|
| FAI | Proves the first production-representative unit matches the released data | New product, new revision, tooling change, or production restart |
| PFMEA | Predicts process failure modes and assigns controls before defects occur | NPI, automotive-style programs, or complex mixed-technology PCBA |
| Control Plan | Turns risk review into specific inspection, test, and reaction steps | Pilot build, bridge production, and recurring production transfer |
| 8D Report | Documents containment, root cause, correction, and recurrence prevention | Customer complaint, lot escape, repeat defect, or supplier corrective action |
| Inspection Records | Show what was checked, by which method, and against which revision | Lot release, customer audit, or internal yield review |
The practical trade-off is cost versus risk. A simple 20-board prototype may only need inspection photos and test results. A 2,000-unit industrial PCBA with BGA packages, firmware loading, and customer audit requirements benefits from a formal FAI package, defined control plan, and 8D response path before release.
PCBA Quality Assurance Workflow
The workflow is designed around release decisions. Each step creates evidence that a buyer, quality engineer, or procurement team can use before approving the next build stage.
Quality requirements intake
We review the released data package, buyer quality clauses, workmanship class, test expectations, and approval flow before the build starts.
Risk review and control plan
Engineering identifies critical packages, known process risks, inspection gates, and reaction plans so PFMEA items connect to real production controls.
First article build and evidence capture
The first production-representative boards are assembled, inspected, tested by plan, and documented before the remaining quantity is released.
Lot containment and corrective action
If a defect appears, suspect boards are contained, root cause is separated from escape cause, and an 8D-style corrective action path is documented.
Release review and repeatability setup
Approved evidence, deviations, test results, and build notes are organized so the same controls can be repeated on the next production lot.
Representative Production Scenario
A typical NPI transfer might include 5 first article PCBAs from a 300-unit pilot lot. The release package would compare the boards against the released BOM, centroid file, assembly drawing, IPC-A-610 workmanship criteria, AOI output, X-ray images for BGA locations, and functional test results supplied by the buyer.
If one board shows a repeated polarity error, production should hold the remaining quantity while the team checks feeder setup, polarity marking, AOI rule coverage, and operator instruction. That decision costs time in the pilot build, but it prevents the same error from multiplying across the lot.
"A first article report is useful only when it changes the release decision. If the report cannot show revision, criteria, evidence, and signoff, it is not protecting the buyer."
Hommer Zhao
Founder & General Manager, PCBInsider
Real SMT First Article Inspection (FAI) Report
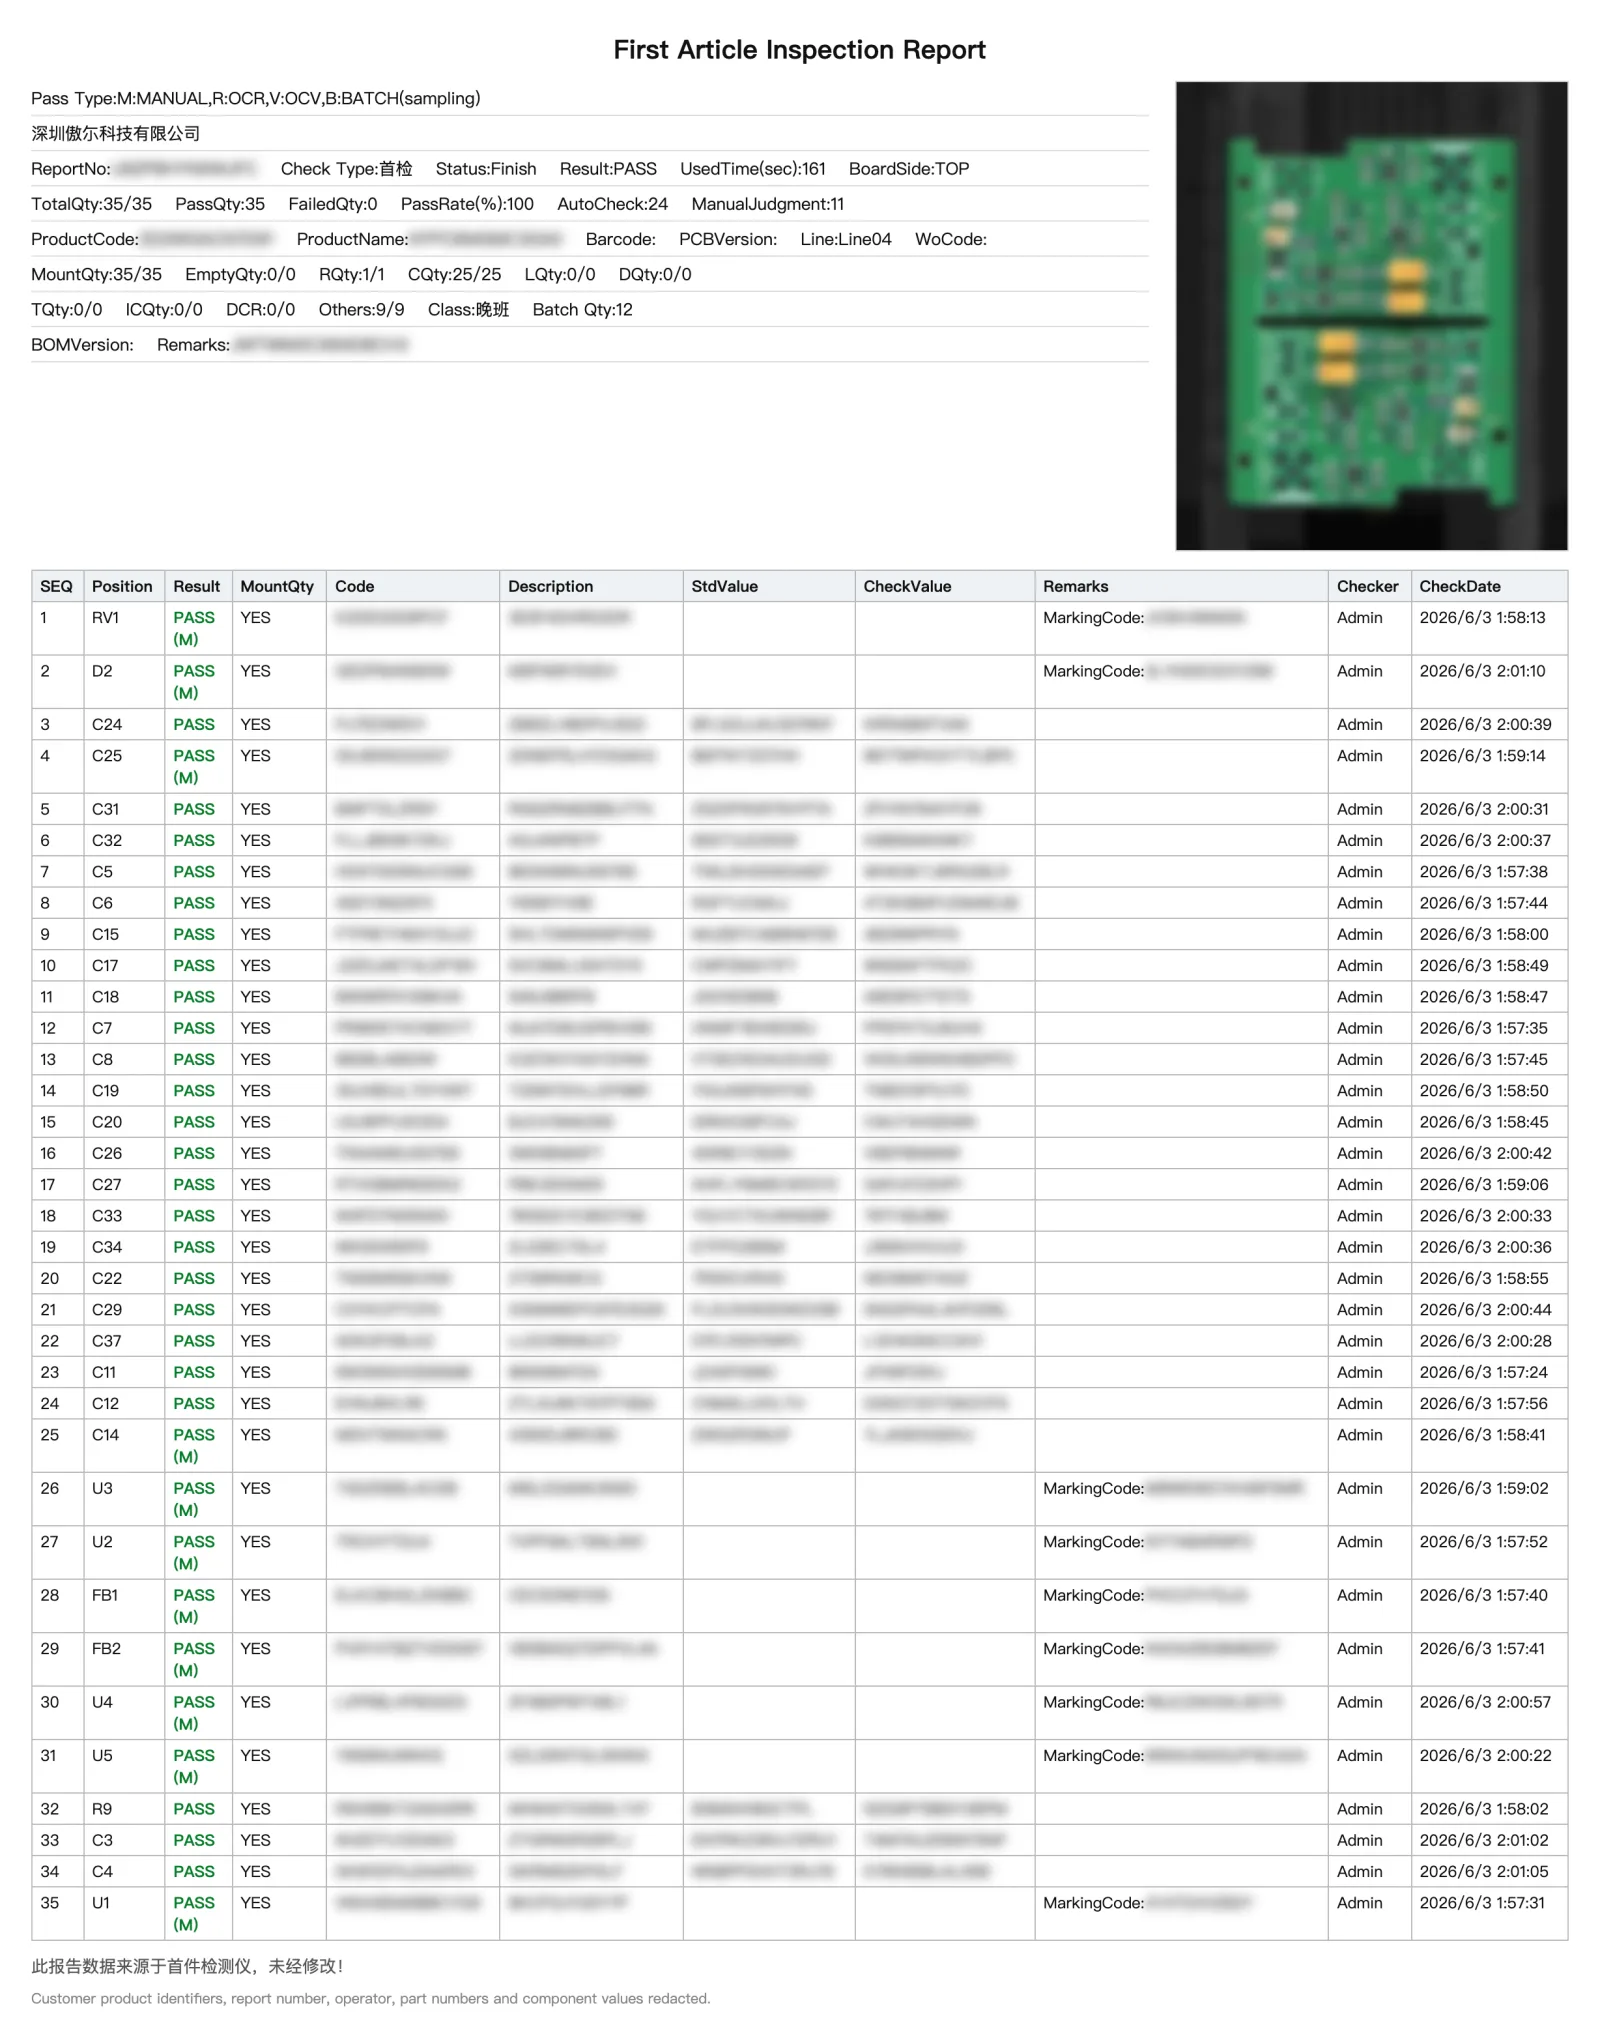
The scenario above is illustrative; the two reports below are real. They come from SMT Line04 at Shenzhen Aoer Technology (深圳傲尔科技有限公司), a sister company in our group, on 3 June 2026: one first-article check for the top side and one for the bottom side, each run on a first-article tester. Customer product identifiers, the report number, part numbers and component values are redacted; every other field and every pass/fail verdict is exactly as the tester printed it.
| Side | Placements checked | Result | Auto / manual judgment | Inspection time |
|---|---|---|---|---|
| Top | 35 | 35/35 PASS | 24 auto · 11 manual | 161 s |
| Bottom | 30 | 30/30 PASS | 25 auto · 5 manual | 142 s |
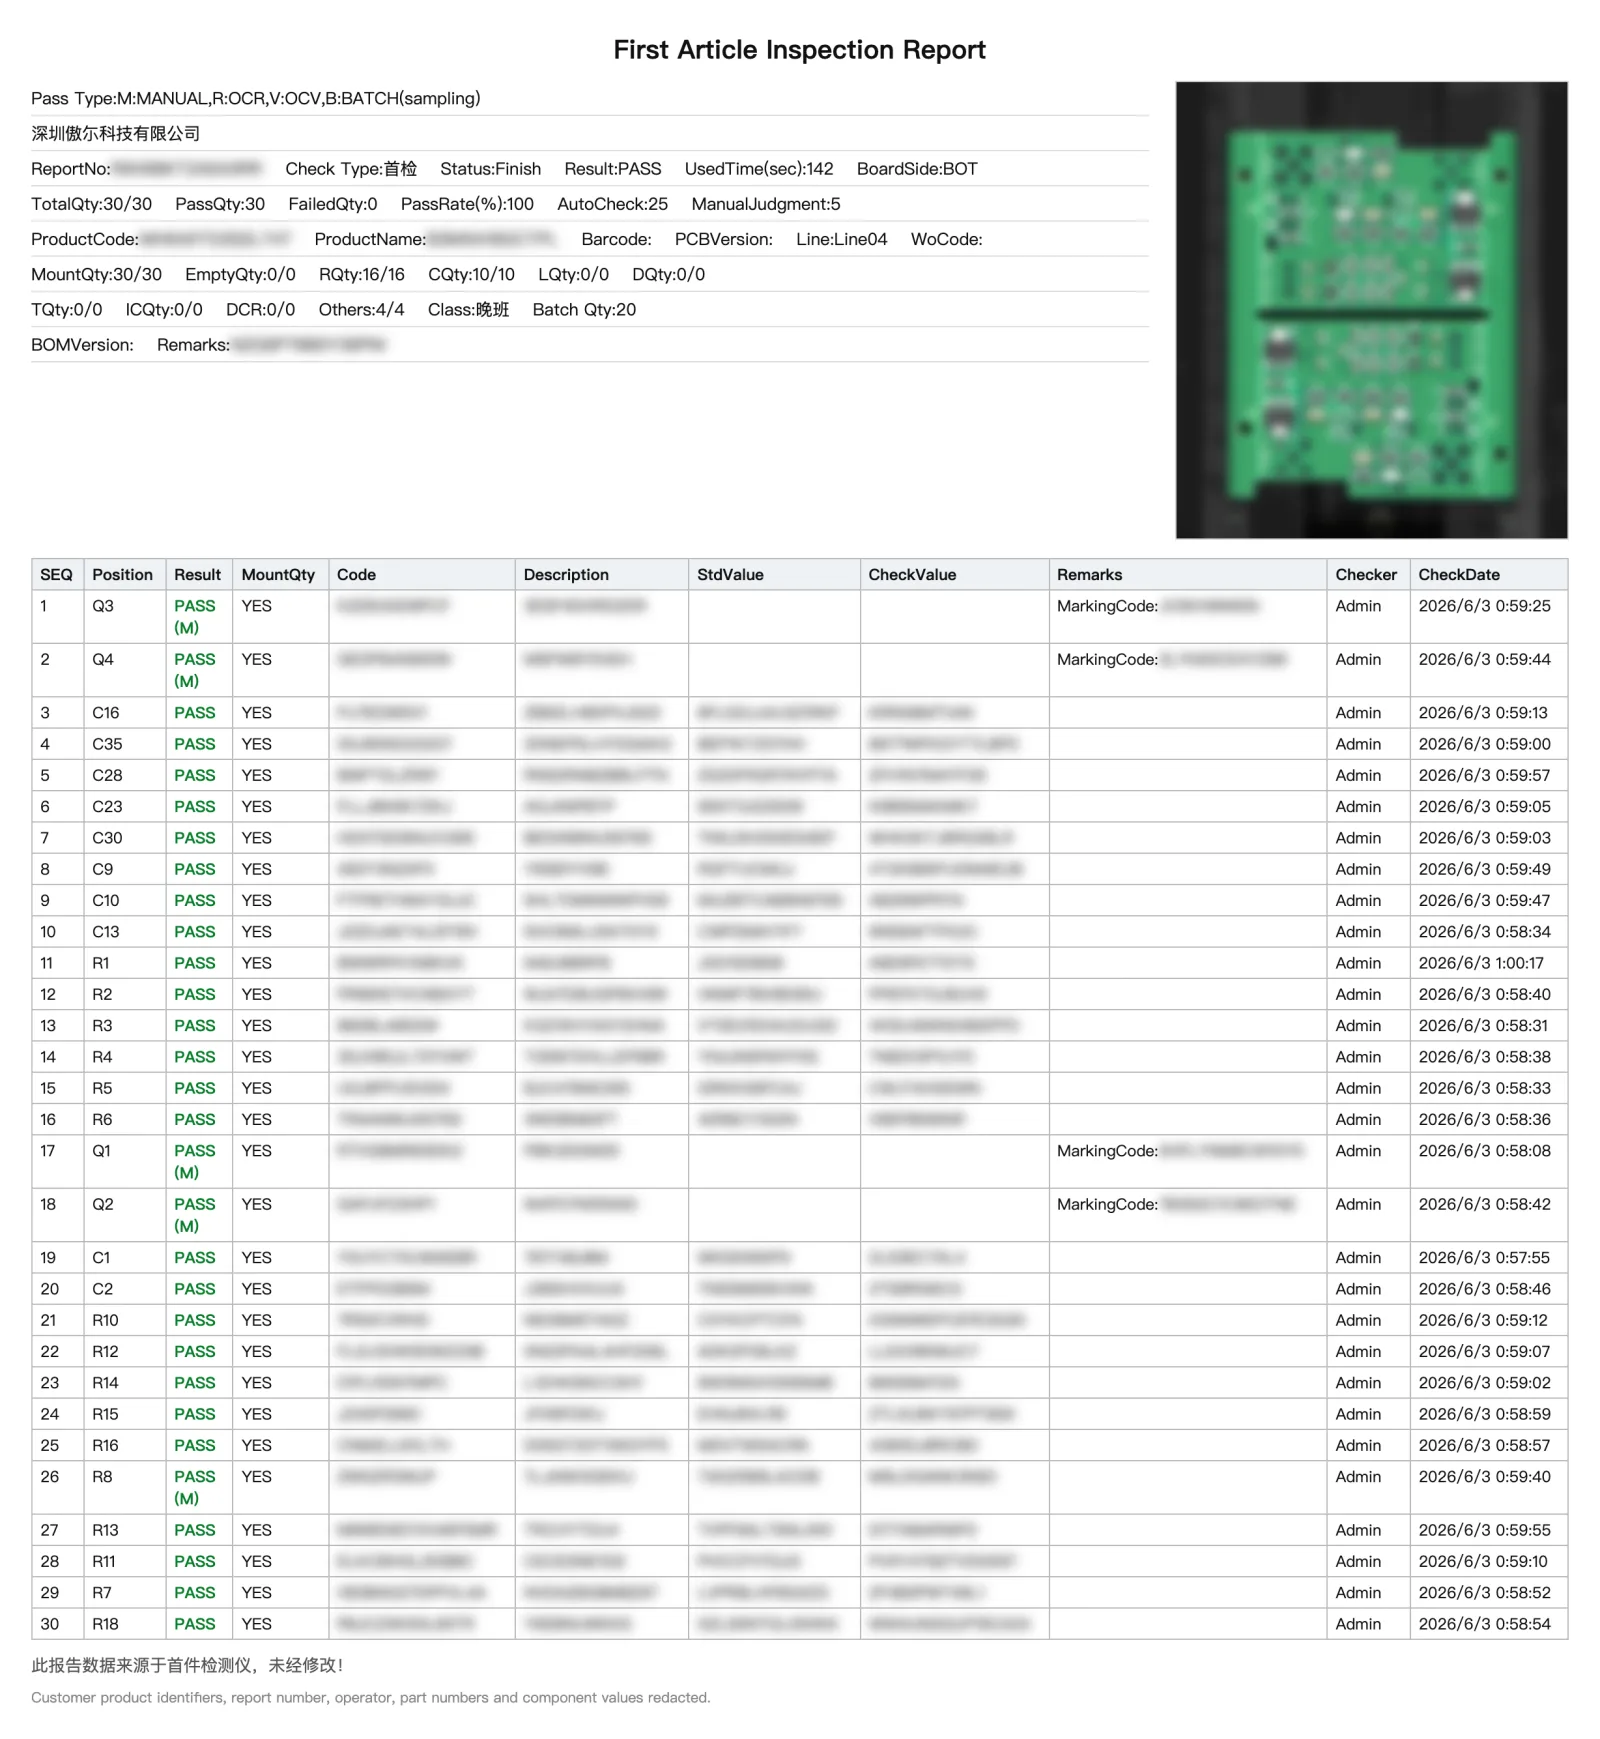
What the report records
- One line per reference designator (RefDes): whether the part was placed (MountQty) and the verdict.
- For resistors and capacitors, the BOM standard value (StdValue) next to the measured value (CheckValue); these values are redacted in the images.
- References without a nominal value (U, D, FB, Q: ICs, diodes, ferrite beads, transistors) are checked by the inspector against the part marking and marked PASS (M).
- Every verdict carries the inspector and a time stamp to the second, so you can see who checked the first article and when.
FAI vs prototype test vs in-line inspection
A prototype test proves the design works. FAI proves that the production setup (feeders, placement program, BOM revision) builds the board you approved, and it runs once at the start of a lot or after a change to the BOM, board revision or program. In-line checks such as AOI keep running on every board for the rest of the lot.
This report covers placement and component values. If you need FAI with dimensional, visual, electrical or functional results, say so in your quote request and we will agree the scope and format with you.
Public References for Quality Terms
These stable public references explain the quality methods behind the service without relying on standards-store pages that often block automated access.
First article inspection
Public background on first article inspection and why production-representative evidence matters before release.
8D problem solving
Overview of the 8D corrective action structure used for containment, root cause, and recurrence prevention.
Failure mode and effects analysis
Reference for FMEA methods used to identify failure modes, effects, causes, and control priorities.
IPC electronics standards context
Public background on IPC as the standards body associated with electronics assembly workmanship references.
Related PCB Assembly Quality Services
Quality assurance depends on the manufacturing and inspection methods around it. These services are commonly linked in the same quote package.
PCB Assembly (PCBA)
Board-level SMT, through-hole, and mixed assembly where quality planning starts before the first article.
Learn morePCB Assembly DFM Review
Pre-production DFM/DFA screening for Gerber, BOM, centroid, stencil, test access, and first article blockers.
Learn moreAOI Inspection Service
Visible-defect inspection that supports first article review and lot-level process feedback.
Learn moreX-Ray Inspection Service
Hidden-joint inspection for BGA, QFN, and bottom-terminated packages that optical inspection cannot verify.
Learn moreFlying Probe Testing Service
Fixtureless opens, shorts, selected value checks, and DFT feedback for prototype and low-volume PCBA release.
Learn moreConformal Coating Service
Protective coating support when release evidence, masking control, and UV inspection need to happen after PCBA approval.
Learn moreICT Testing Service
Fixture-based electrical screening for shorts, opens, polarity issues, and repeat production test control.
Learn moreTest Fixture PCB
Controlled fixture PCB builds that connect DFT access, probe hardware, and production test records.
Learn moreBuyer Guides That Support Quality Planning
PCBA quality assurance works best when the purchase package names the release gate, test method, and reaction plan before the build starts. These PCBInsider guides help buyers define those inputs.
First Article Inspection for PCB Assembly
Buyer guide for defining FAI triggers, evidence, sample count, and approval controls before a production lot is released.
Read guideDFM vs DFT in PCB Assembly
Explains how manufacturability and testability reviews reduce quality risk before AOI, ICT, or functional test gates are selected.
Read guideFlying Probe vs ICT for PCB Assembly
Compares electrical test coverage, fixture cost, volume thresholds, and where ICT belongs in a PCBA control plan.
Read guidePCBA Quality Assurance FAQ
These questions cover the documentation, test, and release issues buyers usually clarify before approving a production build.
What should a PCBA first article inspection report include?
A PCBA first article inspection report should include the PCB revision, BOM revision, centroid data status, assembly drawing review, polarity checks, solder-joint inspection, measurement or photo evidence for critical features, test results, deviations, and approval status. For an IPC-A-610 Class 2 or Class 3 build, the report should identify which workmanship criteria were used instead of saying only visual OK. Buyers should also ask whether the FAI was performed on a production-representative setup, because a hand-built sample does not prove the real line can repeat the result.
I need 200 PCB assemblies for an industrial controller. Is FAI too much documentation?
FAI is usually worthwhile for a 200-unit industrial PCBA if the board has fine-pitch ICs, polarity-sensitive parts, programmed devices, or a high cost of field failure. The report does not need to become a large automotive PPAP package, but it should prove that the first boards match the released BOM, placement data, solder criteria, and test plan before all 200 units are completed. A practical approach is to approve 1 to 5 first article boards, hold the remaining lot, and release production only after buyer signoff.
How does an 8D report differ from normal rework notes?
An 8D report is a structured corrective action record, while rework notes usually describe only what was fixed on a board. A useful 8D for PCB assembly identifies the problem, contains affected units, finds root cause, explains why the defect escaped detection, defines permanent corrective action, and verifies effectiveness on a later lot. For example, replacing one reversed diode is rework; updating feeder verification, AOI polarity rules, and first article signoff is corrective action.
When should PFMEA be used for PCB assembly quality assurance?
PFMEA should be used when the assembly process has enough risk or repeat volume to justify formal prevention planning. Automotive, medical, industrial control, robotics, and telecom PCBAs often benefit because the same soldering, placement, programming, and test risks repeat across lots. PFMEA is most useful before NPI release, not after a defect occurs. The output should drive the control plan: SPI for paste risk, AOI for visible placement risk, X-ray for hidden joints, and ICT or functional test for electrical risk.
Can PCBA quality assurance replace AOI, X-ray, or ICT testing?
PCBA quality assurance does not replace AOI, X-ray, or ICT; it decides how those controls should be used. AOI catches visible defects, X-ray reviews hidden joints, and ICT screens accessible electrical faults. Quality assurance connects the methods to released requirements, risk level, acceptance criteria, and reaction plans. A board with 0.4 mm pitch BGA and no functional test needs a different control plan than a simple through-hole relay board, even if both are PCB assemblies.
What files should I send for a quality-controlled PCBA quote?
Send Gerber or ODB++ files, BOM with manufacturer part numbers, centroid data, assembly drawing, test requirements, approved alternates, workmanship class, and any customer quality clauses. If your buyer requires FAI, 8D response time, PFMEA, control plan, serialization, or certificate of conformance, include those expectations before quoting. Missing quality requirements often create price and schedule changes after the first lot is already in motion.
What is outside the scope of your PCBA quality assurance service?
PCBA quality assurance covers manufacturing release evidence, inspection planning, documentation, containment, and corrective action for the assembly process. It does not replace product safety certification, regulatory approval, medical device validation, automotive homologation, or buyer-owned design verification. PCBInsider can support the manufacturing records needed for a buyer audit, but the product owner must define final compliance requirements and acceptance responsibility.
Need PCBA Quality Records Before Releasing Production?
Send your PCB data, BOM, test plan, and customer quality clauses. We can quote the assembly scope together with FAI, inspection records, PFMEA/control-plan support, and 8D response requirements.