Connector Crimping and Soldering Services for Failure-Prone Interfaces
PCBInsider controls the small termination details that decide whether a connector survives production, test, and field use: terminal fit, solder wetting, cavity position, pull strength, strain relief, and 100% electrical test where the program requires it.
Where this service fits in the manufacturing plan
Connector crimping and soldering services sit between design intent and finished product reliability. A harness drawing may call out a Molex, TE, JST, Deutsch, Amphenol, or customer-specified connector, but the assembly still fails if the terminal range, crimp tooling, solder heat, cavity map, or strain relief is wrong. This page covers that termination-specific work; broader connector selection belongs on our wire harness connectors page.
Crimp Setup Review Before Release
Connector crimping starts with matching the terminal, conductor size, insulation diameter, strip length, and applicator setup.
Solder-Cup and PCB Connector Soldering
Soldered connector work is controlled around wetting, heat exposure, strain relief, and inspection access.
Pull, Continuity, and Polarity Checks
Termination quality has to be proven, not assumed. Production plans can include pull-force checks, cavity verification, continuity, short-circuit screening.
Connector Housing and Cavity Control
Correct crimping still fails the product if terminals are inserted into the wrong cavity or left partly seated.
Strain Relief and Flex-Risk Review
Crimped and soldered terminations need the mechanical load removed from the electrical joint.
Integrated PCBA, Harness, and Box Build Fit
Many connector failures show up only when PCBAs, cables, panels, and enclosures meet.
Capability scope and limits
The strongest RFQ packages define the connector, wire, test, and environment together. We support controlled termination work as part of an assembly program, while substitutions, field repairs, and loose connector resale need a separate review.
- Service focus
- Connector crimping, soldering, terminal insertion, cavity verification, and termination inspection
- Best-fit assemblies
- Wire harnesses, cable assemblies, PCB connectors, panel wiring, box build subassemblies, and NPI prototypes
- Crimp scope
- Open-barrel terminals, closed-barrel contacts, ferrules, ring terminals, quick disconnects, and connector-specific contacts by review
- Solder scope
- Solder-cup connectors, through-hole connector pins, wire-to-board joints, tinned wire ends, and selected coaxial contacts by review
- Quality controls
- Tool setup review, strip-length checks, crimp-height or pull checks by program, solder wetting review, and cavity mapping
- Testing path
- Continuity, shorts, polarity, insulation resistance, hipot, functional fixture testing, and visual inspection as specified
- Documentation needed
- Drawing, wire list, connector part numbers, terminal callouts, pin map, quantity, test requirements, and environmental notes
- Out of scope
- Loose connector resale without an assembly program, uncertified field repairs, and unsupported substitutions without buyer approval
Crimping vs. soldering decision guide
Crimped termination
Best fit: Repeat harness and cable builds where approved tooling can form a gas-tight mechanical joint.
Watch out: Wrong terminal range, worn tooling, over-stripping, and incomplete cavity seating can create intermittent faults.
Soldered termination
Best fit: Solder-cup connectors, PCB-mounted connectors, prototypes, selected coax contacts, and low-volume assemblies requiring direct metal joining.
Watch out: Excess heat, cold joints, solder wicking, flux residue, and missing strain relief can reduce service life.
Hybrid approach
Best fit: Programs where different interfaces in the same product need different termination methods.
Watch out: Mixing methods without clear work instructions makes inspection criteria and rework decisions inconsistent.
The practical rule is simple: use the method the connector, conductor, production volume, and inspection plan can support repeatably. Crimping and soldering are both valid when the work instruction, tooling, and strain-relief plan match the real product.
Inspection evidence buyers should ask for
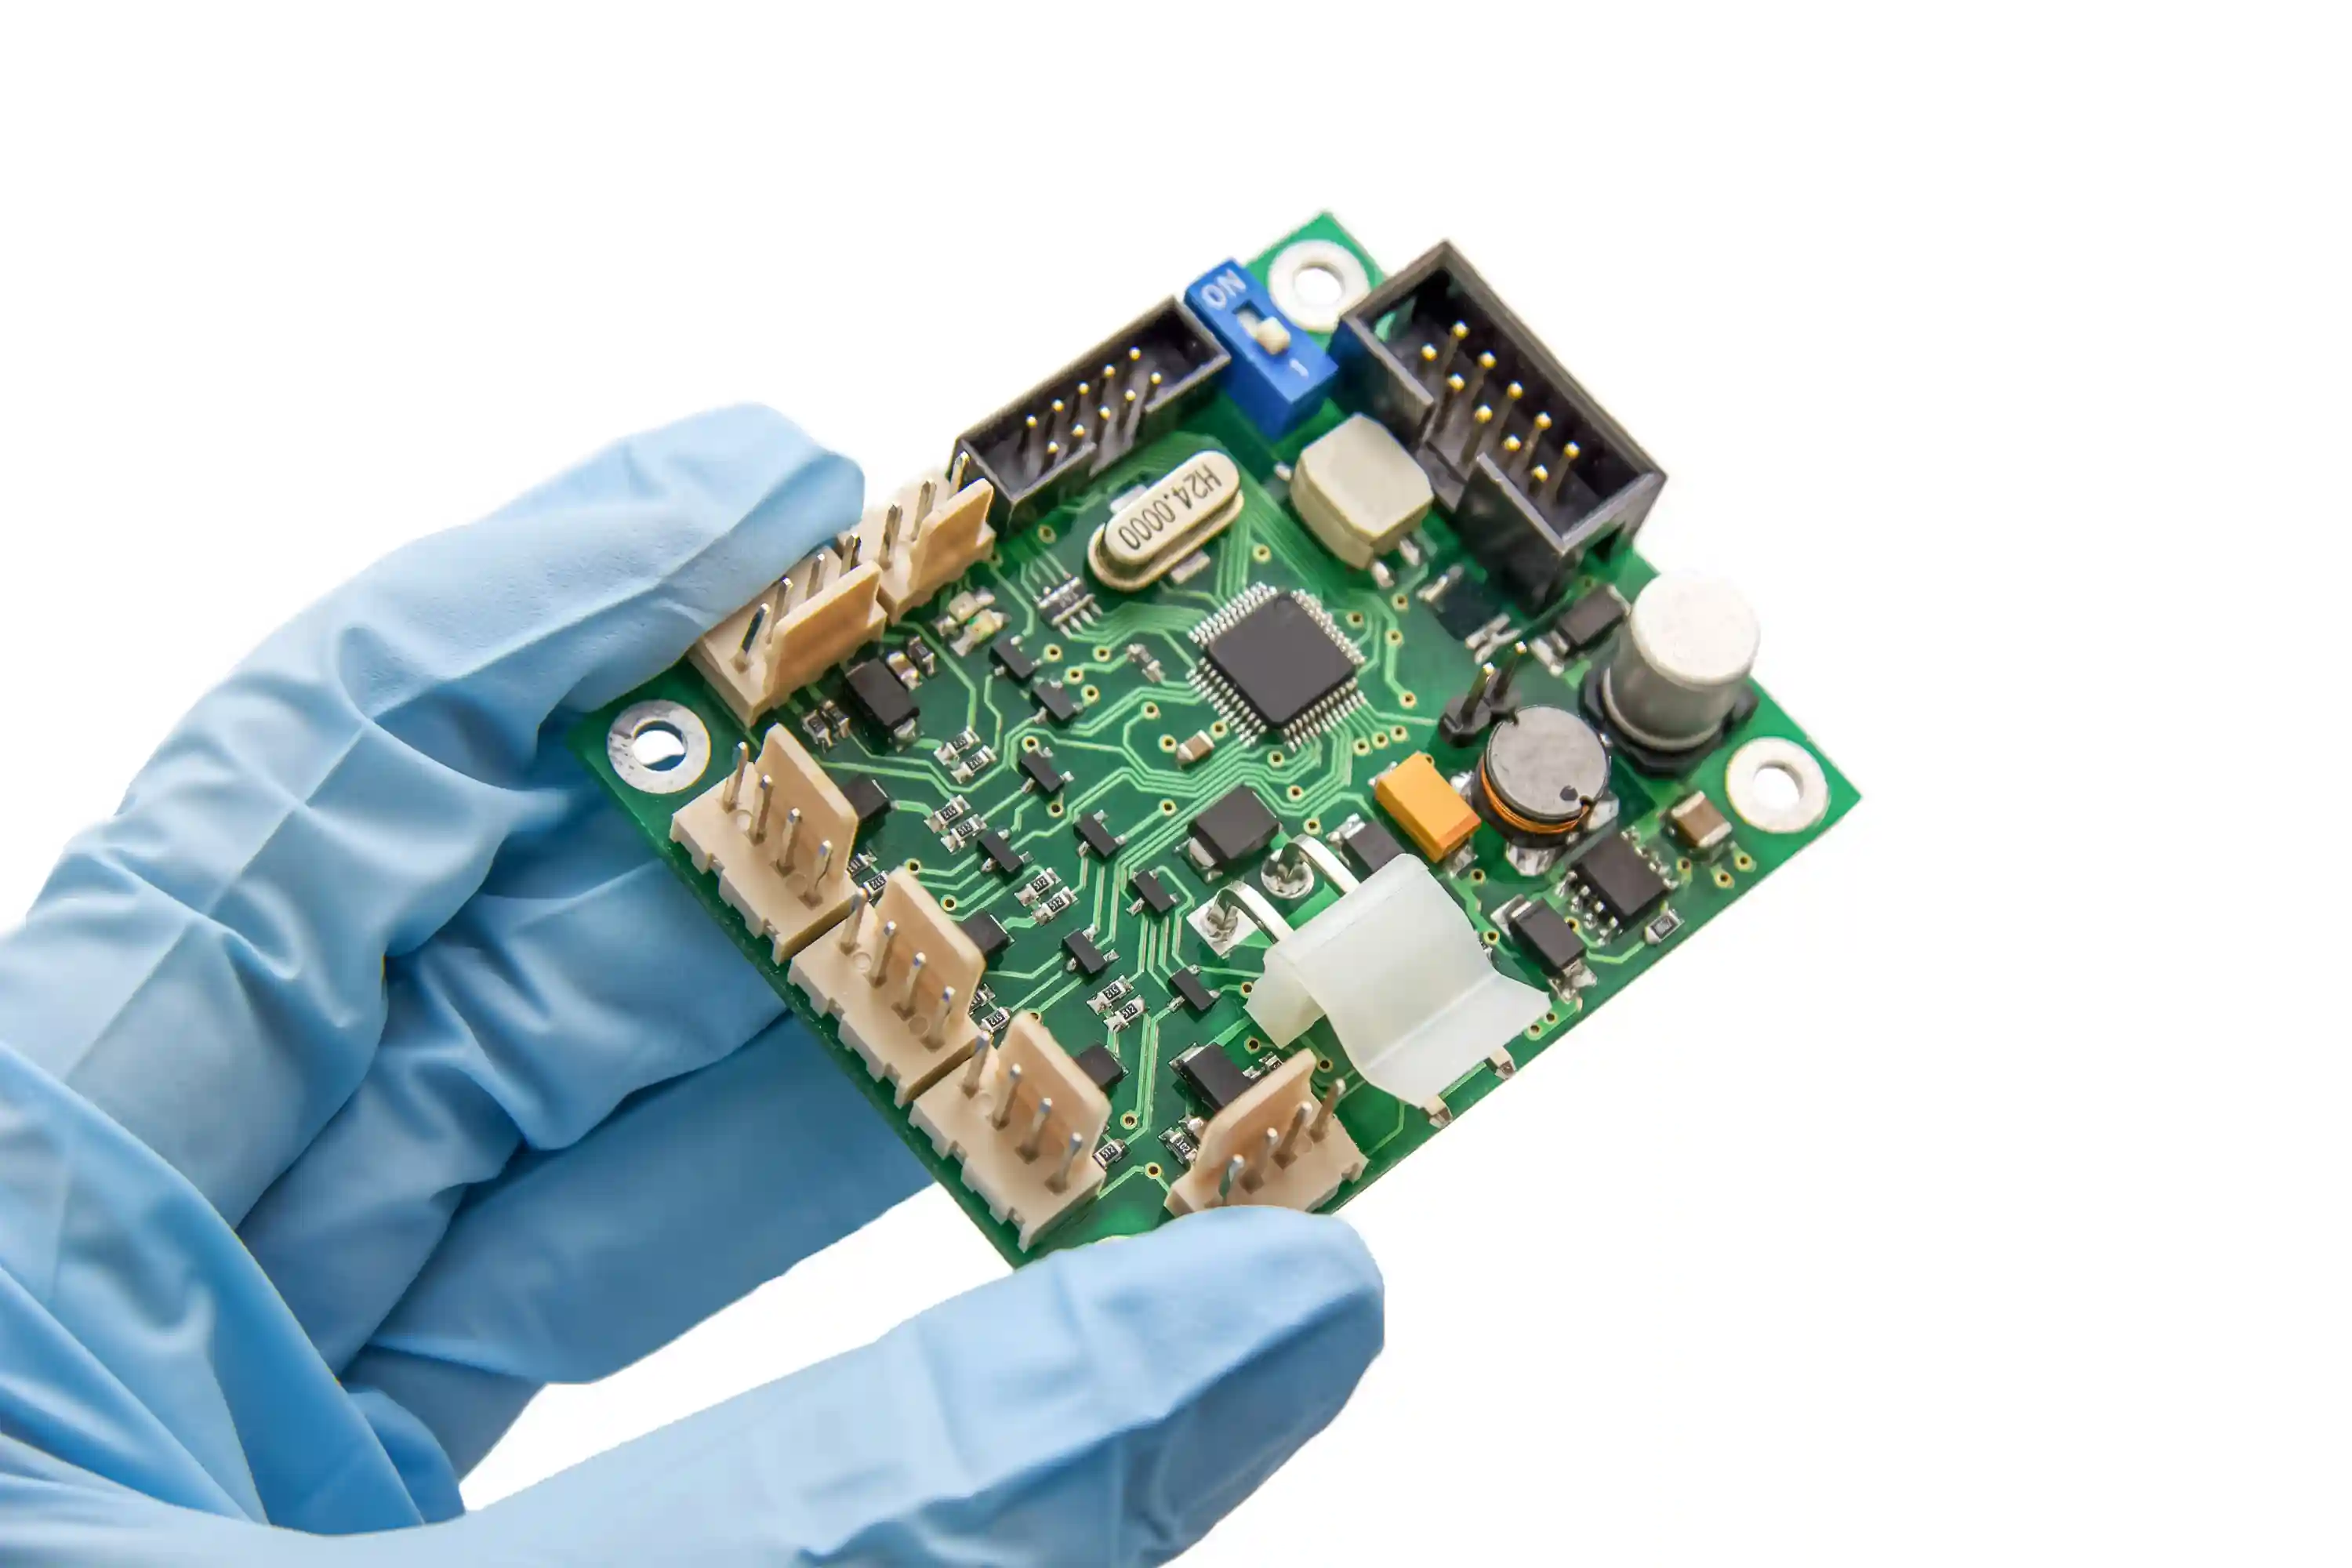
Connector termination quality becomes credible when inspection is tied to named criteria and the actual interface. Background references on crimp joining, soldering, and electrical connectors are useful, but the RFQ should ask how the supplier will verify your exact contact, cavity, wire gauge, and solder joint.
Released drawing and pin map used at the assembly station
Defined strip length, terminal, tool, solder, and inspection criteria
First-article review before repeat production
Continuity, polarity, and short-circuit testing against the approved map
Production workflow
Termination work is released only after the connector package is clear enough to build and inspect consistently. That front-end control prevents late ECOs from becoming hidden production risk.
Review connector and wire data
We check connector series, terminal contacts, wire gauge, insulation diameter, pin map, mating side, expected current, environment, and quantity.
Select the termination method
Crimping is preferred for many repeat harness contacts when tooling is defined.
Build first articles
First articles confirm strip length, crimp geometry, solder fillet shape, cavity position, strain relief, and test coverage.
Run controlled production
Operators work from revision-controlled instructions with connector orientation, pin assignment, tool setup, inspection points, and packaging requirements.
Inspect and test the finished assembly
Finished assemblies receive the electrical and visual checks defined for the program, then ship with records appropriate to the build risk, quantity.
Applications for termination-focused support
PCB assemblies with through-hole headers, board-edge connectors, terminal blocks, and power-entry interfaces
Wire harnesses for industrial controls, robotics, vehicles, energy systems, and medical or laboratory equipment
Custom cable assemblies with circular connectors, D-sub, RJ45, coaxial, sealed, or customer-specified interfaces
Box build programs where internal wiring, panel connectors, PCBAs, fans, switches, and power supplies meet inside one enclosure
Related services and references
Wire Harness Connectors
Use this page when connector-family selection, mating interface, or sealed connector planning is the main issue.
Custom Cable Assembly
Use this service when the termination work is part of a complete cable assembly build.
Through-Hole PCB Assembly
Use this page when connector soldering is part of a mixed SMT and THT PCB assembly.
Box Build Assembly
Use this service when connectorized wiring, PCBAs, and enclosure hardware must ship as one tested system.
Connector crimping and soldering FAQ
These answers cover the questions that usually decide whether a termination project can move from quote to controlled production.
What files do you need to quote connector crimping and soldering services?
A quote is most accurate when the package includes the assembly drawing, connector part numbers, terminal or contact callouts, wire list, pin map, quantities, and test requirements. For PCB connector soldering, include Gerber or ODB++ data, the BOM, and the assembly drawing. For harness work, include wire gauge, insulation type, strip length if known, and any pull-force or hipot requirement. If a design is still early, photos plus a schematic can support a budgetary review, but production release needs revision-controlled documentation.
Should I choose crimping or soldering for my connector assembly?
Crimping is usually the better fit for repeat wire harness production when the correct terminal and tooling are defined. Soldering fits solder-cup connectors, through-hole PCB connectors, some prototype work, and selected contacts where the connector design expects solder. The decision should consider wire gauge, vibration, inspection access, current, strain relief, volume, and whether IPC/WHMA-A-620 or J-STD-001 criteria apply to the released build. A 1000-piece harness program often favors crimp process control, while a 10-piece lab interface may justify soldered contacts.
I need 50 prototype cable assemblies with mixed crimped and soldered connectors. Is that too small?
Fifty prototype cable assemblies is a normal NPI quantity when connector availability and documentation are clear. The main cost drivers are not only labor; tooling setup, first-article inspection, custom fixtures, unusual terminals, and test coverage can matter more than piece count. We can build low-volume mixed-termination assemblies, then keep the same approved materials and work instructions ready if the program moves to 500 or 5000 units. The important step is locking the pin map and termination method before the first article is approved.
How do you inspect crimped connector contacts before shipment?
Crimp inspection can include strip-length verification, conductor brush review, insulation support checks, terminal seating confirmation, cavity map review, pull-force checks by plan, and 100% continuity testing. Some programs also require crimp-height measurements or cross-section review, depending on the contact family and reliability class. The inspection plan is set against the drawing, connector manufacturer requirements, and the risk level of the assembly. For IPC/WHMA-A-620 Class 3 style expectations, incomplete seating, damaged strands, and poor insulation support are treated as release risks.
Can you solder connectors directly to a PCB assembly?
Yes, connector soldering can be included with PCB assembly when the release package defines the connector orientation, solder alloy, inspection criteria, and mechanical support. Through-hole headers, terminal blocks, board-edge connectors, and wire-to-board interfaces are common examples. For heavy connectors, we also review standoff height, mounting hardware, strain relief, and whether selective soldering or hand soldering is the responsible process. If the connector carries mechanical load, solder joints should not be the only structure resisting cable movement during installation or service.
My product fails intermittently after vibration testing. Can termination quality be the cause?
Yes, intermittent faults after vibration often trace back to termination mechanics: weak crimp compression, poor insulation support, incomplete terminal seating, solder wicking into stranded wire, missing strain relief, or connector latch issues. We review the failed interface as an assembly system, not as a loose connector. A practical review checks the terminal, wire gauge, cavity retention, bend direction, pull data, and electrical test evidence. The first containment step is usually comparing the failed sample against the approved pin map, strip length, and termination work instruction.
Need connector terminations reviewed before build release?
Send the connector part numbers, wire list, pin map, drawing, and target quantity. We can quote the crimping, soldering, inspection, and test path as part of your PCB, harness, cable, or box build program.